
Why Choose a Drilling Rig API 6A Check Valve?
Choosing the right Drilling Rig API 6A Check Valve affects pressure control, equipment protection, and daily drilling confidence. These valves manage reverse flow when pumps stop, lines depressurize, or pressure conditions change suddenly. A reliable valve can prevent fluid movement through critical well-control equipment.
“Valve reliability begins with verified materials, correct pressure ratings, and disciplined maintenance,” says Daniel Mercer, an API 6A valve reliability specialist. His point is practical. A valve may look robust on a workshop bench, yet fail when exposed to abrasive mud, vibration, trapped pressure, and repeated cycling.
A Drilling Rig API 6A Check Valve is designed for demanding wellhead and drilling applications. API 6A compliance supports consistent manufacturing, inspection, pressure testing, and traceability. These controls matter when equipment operates under high pressure and limited access.
Picture a rig floor during a pressure test. Gauges fluctuate. Mud gathers around the connection. Operators need a valve that closes cleanly, without dangerous delay or leakage. That performance depends on seat quality, body strength, sealing design, and installation accuracy.
The choice is not only about purchase price. It includes service life, replacement time, maintenance access, and documented test results. Small weaknesses become expensive problems.
No valve is perfect. That deserves honest attention.
Even a certified component needs correct sizing, clean installation, and scheduled inspection. A thoughtful selection process reduces uncertainty, supports safer operations, and helps drilling teams protect valuable equipment in harsh field conditions.
What Is a Drilling Rig API 6A Check Valve?
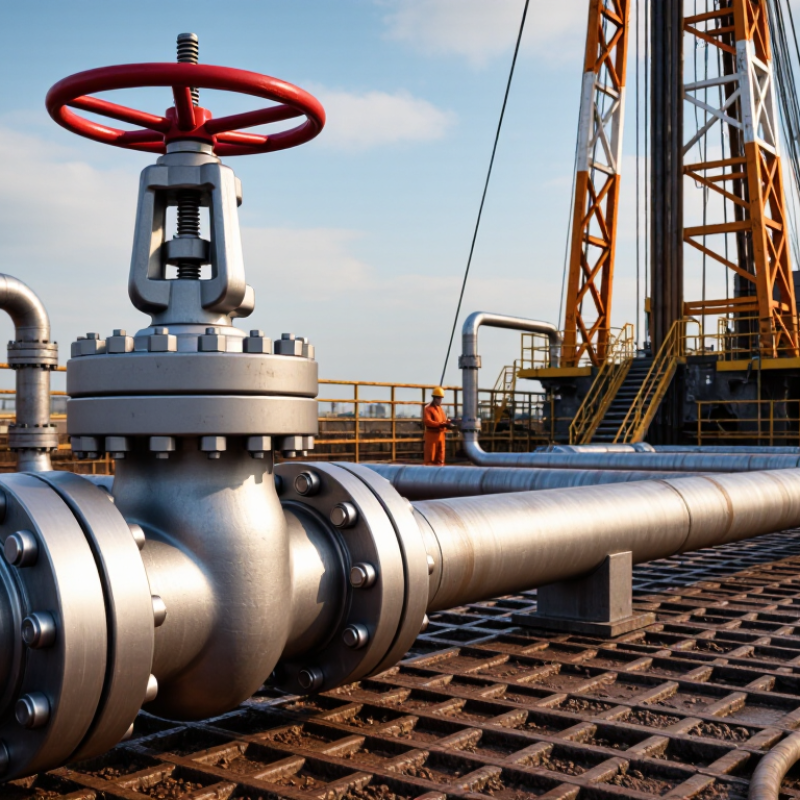
A drilling rig API 6A check valve is a pressure-control component designed to permit fluid flow in one direction only. It automatically limits reverse flow through a wellhead or surface connection. This function helps protect pumps, manifolds, pressure lines, and other equipment from sudden backflow.
The valve usually contains a body, closure element, seat, and pressure-rated connections. When upstream pressure rises, the closure element moves away from the seat. Reverse pressure pushes it closed. Simple in principle. Severe drilling conditions make selection more demanding. Pressure rating, bore size, temperature range, fluid composition, and connection type must match the installation. Material selection also matters when corrosive or sour fluids may be present.
API 6A provides requirements for equipment used in wellhead and tree applications, including pressure integrity, manufacturing controls, testing, and documentation. A reliable check valve should have traceable materials and verifiable pressure-test records. Field experience shows that small seating damage can cause leakage, even when the external body looks normal. That detail is easy to miss. Regular inspection should examine sealing surfaces, bolting, erosion, and signs of vibration. No check valve is maintenance-free. Selection is not always obvious, because the lowest purchase cost may create higher inspection and replacement demands later. Engineers should review operating data, installation conditions, and applicable specifications before choosing a valve for drilling service.
| Data Dimension | Typical API 6A Requirement or Range | What It Means for Drilling Operations |
|---|---|---|
| Valve Function | One-way flow control | A check valve permits drilling fluid, well-control fluid, or other process media to flow in one direction and automatically restricts reverse flow. |
| Applicable Standard | API Specification 6A | API 6A establishes requirements for wellhead and Christmas-tree equipment, including pressure-containing and pressure-controlling equipment used in oil and gas wells. |
| Common Valve Designs | Swing, piston, dart, or axial-flow check valve | The design is selected according to flow direction, pressure drop, solids content, installation position, maintenance requirements, and the required closing response. |
| Nominal Bore Sizes | Approximately 113/16 in to 211/4 in | API 6A equipment is available in a broad range of nominal bore sizes. The exact bore must match the connected wellhead, manifold, choke, kill, or flowline equipment. |
| Rated Working Pressure | 2,000; 3,000; 5,000; 10,000; or 15,000 psi | The selected pressure rating should be equal to or greater than the maximum anticipated surface pressure and must be compatible with every connected pressure-containing component. |
| Pressure Rating in SI Units | Approximately 13.8 to 103.4 MPa | The equivalent pressure range is useful when drilling and well-control specifications are prepared in metric units. Pressure conversions should be verified before procurement. |
| Product Specification Level | PSL 1, PSL 2, PSL 3, or PSL 4 | The PSL identifies increasing levels of manufacturing control, documentation, inspection, and testing. The required level depends on the well program and operator specification. |
| Performance Requirement | PR 1 or PR 2 | Performance Requirement levels define functional and environmental qualification expectations. PR 2 generally involves more demanding temperature and operational qualification than PR 1. |
| Temperature Class | API 6A temperature classes K, L, N, P, R, S, T, U, and V | The temperature class corresponds to a defined operating-temperature range. Selection must account for well temperature, ambient conditions, fluid temperature, and elastomer limitations. |
| Typical Body Materials | Carbon steel, low-alloy steel, or corrosion-resistant alloy | Material selection depends on pressure, temperature, hydrogen sulfide exposure, chloride content, erosion risk, and the applicable sour-service requirements. |
| Sour-Service Consideration | Material compliance may be required for H2S service | For sour wells, metallic materials and hardness controls should be specified in accordance with the applicable sour-service standard and project requirements. |
| End Connections | Flanged, studded, or other API 6A-compatible connections | Connection type, nominal size, pressure rating, flange facing, bolting, and bore dimensions must be identical or properly compatible with the mating equipment. |
| Flow Direction | Clearly marked by an arrow on the body | The flow-direction marking helps prevent incorrect installation and supports reliable backflow protection during drilling, well testing, stimulation, and well-control operations. |
| Leak-Testing Focus | Pressure-containing and closure-member integrity | Testing typically verifies body integrity, seat sealing, pressure-retaining parts, and functional operation in accordance with the applicable API 6A edition and purchase specification. |
| Primary Safety Benefit | Prevents unintended reverse flow | The valve can help protect pumps, manifolds, pressure-control equipment, and personnel by limiting reverse flow and reducing the risk of uncontrolled pressure transfer. |
| Installation Position | Depends on the valve design | Some check valves are suitable for horizontal or vertical installation, while others require a specific orientation for reliable closure. The approved installation orientation must be confirmed before use. |
| Maintenance Items | Seat, closure member, seals, body, and fasteners | Inspection intervals should consider operating cycles, abrasive solids, corrosive fluids, pressure spikes, temperature exposure, and the manufacturer’s documented maintenance procedure. |
| Selection Priority | Pressure, bore, temperature, fluid, PSL, PR, and connection compatibility | Choosing an API 6A check valve by pressure rating alone is insufficient. The complete service envelope and interface dimensions must be reviewed before application. |
| Technical note: Actual dimensions, materials, allowable temperature limits, testing requirements, and service restrictions vary by valve design and applicable API 6A edition. Final selection should be confirmed against the approved equipment datasheet and well-control design. | ||