In 2026, choosing Mold Parts suppliers is not simply a price comparison. A low quote can hide long lead times, unclear tolerances, or costly rework. The right partner should understand the part’s function, tool conditions, materials, and inspection needs. Ask for current capability evidence, not polished promises. Review sample components, dimensional reports, material certificates, and revision-control practices. Look closely at fit. A pin that measures correctly on paper may still bind in a hot-running mold.
Manufacturing quality expert W. Edwards Deming is often quoted: “Quality comes not from inspection, but from improvement of the production process.” That principle offers a useful test for suppliers. Can they explain how they prevent repeat defects, manage process changes, and respond when a batch falls outside specification? Request clear answers about machining capacity, surface finish, packaging, delivery updates, and corrective actions. Then compare their evidence against your actual operating conditions. Not just a brochure. A short technical review can reveal whether the supplier asks thoughtful questions or merely agrees with every requirement. I would also leave room for doubt: one successful sample does not prove consistent production. Check references where possible, confirm details in writing, and set a measured qualification plan. Reliable Mold Parts sourcing depends on repeatable results, honest communication, and fit-for-purpose verification. Not the lowest number alone.
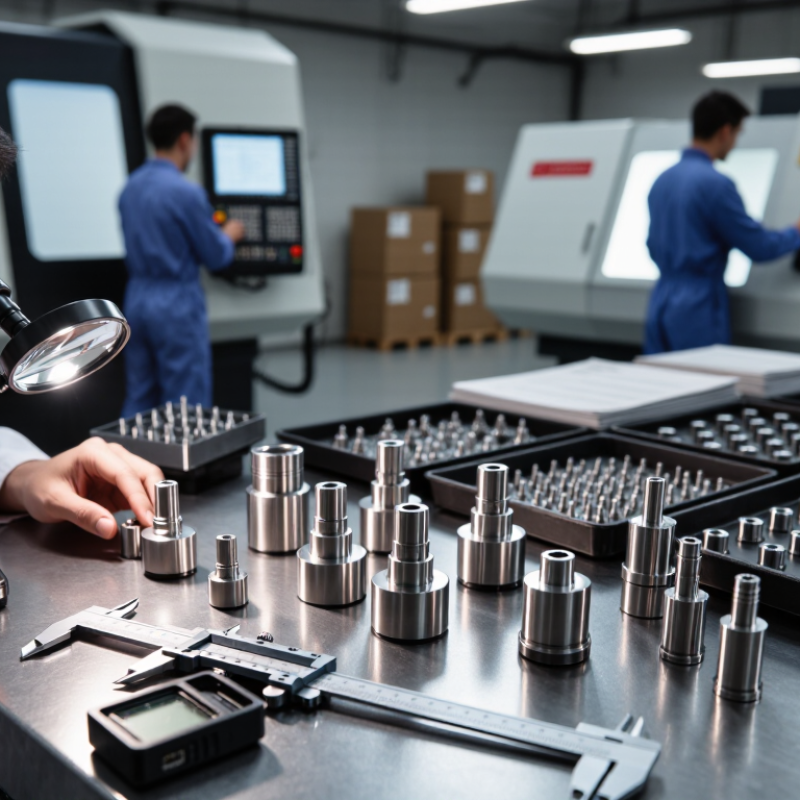
Start with the mold’s operating conditions, not a catalog number. Record the part’s function, resin, machine tonnage, cycle temperature, and expected shot count. Specify steel grade, hardness, surface finish, critical dimensions, and allowable tolerances. Add a drawing with datum references, plus photographs of wear-prone areas. For cooling components, state the connection size and pressure-test requirements. For slides and ejectors, define fit, lubrication, and replacement frequency. Small omissions matter. A supplier cannot quote risk accurately when “standard fit” means different things to each shop.
Then score suppliers against measurable criteria: dimensional inspection capability, material traceability, sample approval, change control, lead-time performance, and corrective-action response. Ask for inspection records from comparable parts, not just a capability brochure. ISO’s 2022 Survey reported 1,265,216 ISO 9001 certificates worldwide; certification signals a quality system, but does not prove a specific mold part will meet your drawing. Request a first-article report and agree on how critical dimensions will be measured. A clean audit can still miss a recurring burr on a vent edge. No scorecard removes every risk, either. Leave room for a small trial order, and review actual fit, wear, and delivery records before expanding the supplier’s scope.
How to Choose Mold Parts Suppliers in 2026?
Assess Manufacturing Capabilities and Technical Compatibility
Choosing a mold parts supplier starts with checking whether its processes fit your part, not just its catalog. Ask what machining methods it uses and which tolerances it can consistently hold. For example, a tight-fitting ejector pin may need closer inspection than a standard guide component. Request sample inspection records, including measured dimensions and the tools used. A polished brochure is not proof.
Review the supplier’s equipment, inspection process, and material traceability. Ask how it handles a drawing revision after production has started. The answer can reveal whether engineering, machining, and quality teams share current specifications. If possible, compare a sample part with your drawing using a coordinate measuring machine or suitable gauges. Small gaps matter. One overlooked datum can affect alignment during assembly.
Technical compatibility includes more than dimensions. Confirm steel grade, hardness, surface finish, heat-treatment requirements, and fit with existing mold assemblies. Share relevant drawings and operating conditions early, while protecting confidential design details through clear written procedures. A supplier may meet the stated tolerance yet struggle with your assembly sequence; discuss that risk directly. No process is perfect, and test-fitting a first article may uncover assumptions neither side noticed. Ask who will review those findings and how changes will be documented.
ISO 286 standard tolerance values for nominal dimensions over 30 mm and up to 50 mm are shown for reference. When assessing a supplier, compare the tolerances your mold design requires with documented process capability and inspection results. These standard tolerance grades are not a guarantee of any supplier’s achievable accuracy.
In 2026, a mold parts supplier should be able to explain how quality checks work on the shop floor. Ask to see inspection plans, equipment calibration records, and examples of how defects are handled. A certificate alone tells you little about daily practice. During a visit, compare a measured part with its inspection report and drawing. Paper can look tidy.
Check that material grades match your specifications, not just a supplier’s standard offering. Request mill or batch certificates linked to the actual steel, aluminum, or resin used. For critical dimensions, ask how the supplier measures them and how often gauges are checked. A clear answer should include real details, such as the instrument, inspection frequency, and acceptance limits. Vague confidence is not evidence.
Traceability should connect each part to its material lot, production date, machine, and inspection results. Ask the supplier to trace a sample component backward through those records. If a mold insert is reworked, the revision and approval should also be recorded. No system is perfect. I would still check how staff handle missing data, because that is where polished procedures can fail. A small pilot order can reveal whether records stay accurate under normal production pressure.
Choosing mold parts suppliers in 2026 means comparing the full delivery picture, not just the quoted unit price. Ask for lead times by process and part type, then check recent on-time delivery data against your own order history. A four-week estimate means little if it excludes tooling adjustments, inspection, or shipping. Compare total landed costs, including packaging, freight, and the cost of carrying extra stock. A low quote can still be expensive.
Resilience matters when a machine goes down or a material shipment slips. Ask whether the supplier has backup equipment, documented capacity, and alternative material sources. McKinsey’s 2020 global supply-chain survey found that 93% of respondents planned to make their supply chains more resilient. That is a useful signal, not a guarantee of delivery. Check how the supplier handles disruptions, and request clear update intervals. Forecasts can be wrong. So can a polished scorecard.
Tips: Request a sample schedule showing order, production, inspection, and dispatch dates. Compare quotes using the same specifications and delivery terms. Ask for evidence of recent lead-time performance, not only a best-case estimate. Keep the comparison practical; a spreadsheet cannot capture every production risk.
A polished sample is only a starting point. Ask the mold parts supplier to produce trial pieces on the intended machine, using the proposed resin, tooling, and process settings. Measure critical dimensions across several shots, not just one attractive part. Check flash, sink marks, gate vestige, warpage, and cavity-to-cavity variation. Keep the results, measurement method, and approved sample together as a clear reference.
Audit the process behind those parts. Review calibration records, material traceability, maintenance logs, inspection plans, and how process changes are approved. Then walk the production area and compare written procedures with actual work. Small details matter. A tidy audit file cannot prove that operators follow the same settings each shift. McKinsey Global Institute’s 2020 report on global value chains estimated that disruptions could erase 45% of one year’s profits over a decade. That risk makes repeatable controls more valuable than a low quote alone.
Use the audit to test evidence, not to collect paperwork. Ask the supplier to show recent inspection data for the same part family, explain out-of-tolerance results, and demonstrate corrective actions. One weak point is easy to miss: a supplier may prepare a special sample run that does not reflect normal production. Schedule a follow-up check during routine manufacturing, and compare those parts with the approved sample before releasing larger orders.
Practical validation checklist. Targets below are suggested starting points; confirm tolerances, material requirements, and acceptance criteria against the part drawing and purchase specification.
| Validation Area | What to Check | Suggested Acceptance Criteria | Evidence to Request or Review | Decision Guidance |
|---|---|---|---|---|
| Sample dimensional accuracy | Critical dimensions, datum relationships, hole positions, and fit features on trial parts. | All critical dimensions meet the drawing; non-critical dimensions meet their stated tolerances. | Ballooned inspection report, measurement results, and samples traceable to the production process. | Hold approval if a critical feature is out of tolerance or measurement methods are not identified. |
| Measurement capability | Whether gauges and measuring equipment are suitable for the feature and tolerance being checked. | Equipment is calibrated and appropriate; measurement repeatability is demonstrated for critical checks. | Calibration records, gauge list, measurement method, and repeatability study where risk warrants it. | Request a measurement-system review when results are inconsistent or close to specification limits. |
| Material and heat treatment | Material grade, hardness, heat-treatment condition, and other specified properties. | Results match the purchase specification and applicable material requirements. | Material test certificate, heat-treatment record, hardness results, and lot identification. | Do not release parts if material identity or required properties cannot be traced to the supplied lot. |
| Surface finish and coating | Specified roughness, coating type and thickness, corrosion protection, and visible defects. | Meets the drawing or specification; no defects that affect function, assembly, or service life. | Surface measurement results, coating inspection records, and visual samples under agreed lighting. | Clarify the inspection method and acceptance standard before approving appearance-sensitive parts. |
| Sample-to-process consistency | Whether approved samples were produced using the intended equipment, tooling, and process route. | The sample process is representative of routine production. | Process flow, machine or tool identification, setup records, and sample batch traceability. | Request a production trial if samples were specially made or the planned process has changed. |
| Audit: quality system | Document control, inspection planning, nonconformance handling, corrective action, and record retention. | Processes are documented, consistently followed, and supported by objective records. | Audit checklist, representative inspection records, corrective-action examples, and document revisions. | Require corrective actions for gaps that could affect product conformity or traceability. |
| Audit: production controls | Equipment maintenance, operator instructions, in-process checks, tool control, and change management. | Controls are defined for critical operations and changes are reviewed before implementation. | Maintenance logs, work instructions, process-monitoring records, and change-approval records. | Escalate uncontrolled process changes or repeated production issues before placing routine orders. |
| Traceability | Ability to connect finished parts to material lots, production dates, inspection records, and sub-processes. | Traceability meets the buyer’s specification and applicable regulatory requirements. | Example traveler, lot labels, inspection records, and a demonstrated traceability exercise. | Confirm that traceability can be maintained through subcontracted processes where applicable. |
| Delivery performance | Quoted lead time, capacity assumptions, order confirmation, and communication of schedule risks. | Commitments are realistic, clearly defined, and supported by a capacity or scheduling review. | Written quotation, production schedule example, capacity review, and escalation process. | Compare like-for-like lead times, including tooling, inspection, finishing, and shipping stages. |
| Final approval | Closure of sample findings, audit actions, specification questions, and commercial requirements. | Critical issues are closed; remaining actions have owners and agreed due dates. | Approved sample record, audit action log, final specification, and documented approval decision. | Approve conditionally only when open actions are low risk, documented, and monitored. |
MSIRobot